MAPAL sets a new benchmark for the machining of drive joints
When it comes to machining hardened steel, there is virtually no alternative to PcBN. This is all the more true when machining complex components such as constant-velocity joints. As a long-standing, close partner to manufacturers of drive joints, MAPAL possesses in-depth expertise in this field and, in 2026, will significantly further increase production efficiency for these key components through the targeted development of new cutting material grades and optimisations to tool design.
High demands on the hard machining of CV joints
Depending on the vehicle type, a wide variety of drive joint designs are used in automotive engineering, both on the wheel side and on the gearbox side. The main components include the outer housing, also known as the outer race, the ball hub (inner race) and the ball cage. The balls roll in specially shaped raceways between the inner and outer races and are guided by the cage in such a way as to enable a constant rotational movement even when subjected to a bending angle, such as during a steering manoeuvre.
The ball raceways on both the inner and outer races must be hard-milled. The requirements regarding shape and surface finish are very high at this point, which is why the geometric design of the milling cutter plays a decisive role. MAPAL tailors its ball-track milling cutters precisely to the tolerances required for the component. In addition to the geometry of the tool, the cutting material used and the preparation of the cutting edges are important for tool life, performance and the surface quality achieved.
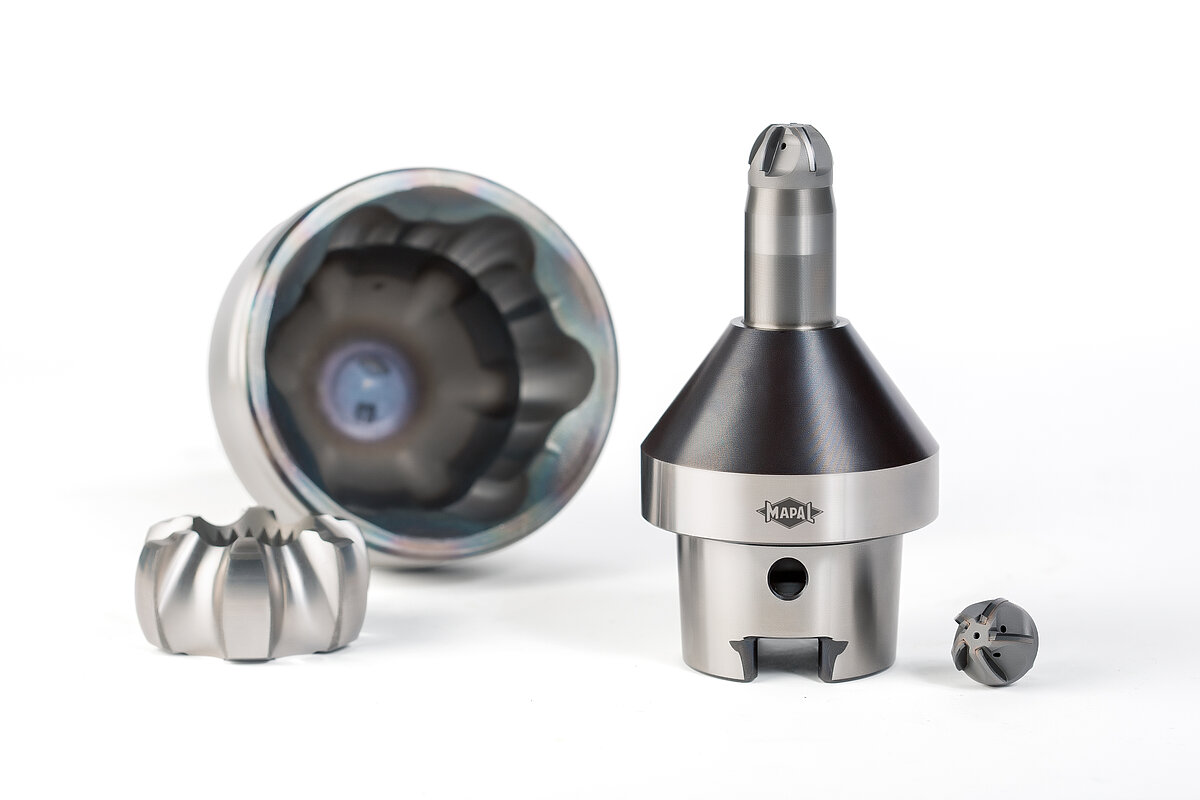
MAPAL is setting a new benchmark with new PcBN cutting materials, tailored to the specific requirements of hard milling of drive joints, combined with a five-fluted milling cutter design
Cutting material development specifically tailored to process requirements
Thanks to its expertise, MAPAL is able to develop cutting materials specifically for the machining of certain components. The new, uncoated PcBN cutting material FU240 is tailored to the requirements of hard milling the ball raceways on the outer race, whilst the FU290 cutting material is tailored to those of the inner race. Different PcBN substrates are generally used to account for the differing machining characteristics of the inner and outer races and the associated wear mechanisms on the tool. Furthermore, the industry uses different materials for the two components. Quenched and tempered steels are used for the outer race, whilst case-hardened steels are generally used for the inner race. Whilst car manufacturers each follow their own philosophy regarding design and, in particular, ball guidance, the materials used are largely standardised.
Significantly higher tool life in milling operations
To successfully improve its PcBN cutting materials and thereby secure its technological lead, MAPAL, as a technology partner, draws on an in-depth understanding of the entire process. To achieve longer tool life when machining CV joints, the aim was to find the optimum balance between high resistance to abrasion and diffusion whilst maintaining sufficient toughness. Development parameters included, amongst others, the CBN content of the cutting material, grain sizes and the composition of the binder. Initial results demonstrate a significant increase in tool life for the new cutting materials: compared with those used previously, the new grades FU240 and FU290 delivered an increase in tool life of more than 30 per cent at cutting speeds in the range of 180 m/min and a tooth feed between 0.07 and 0.10 mm.
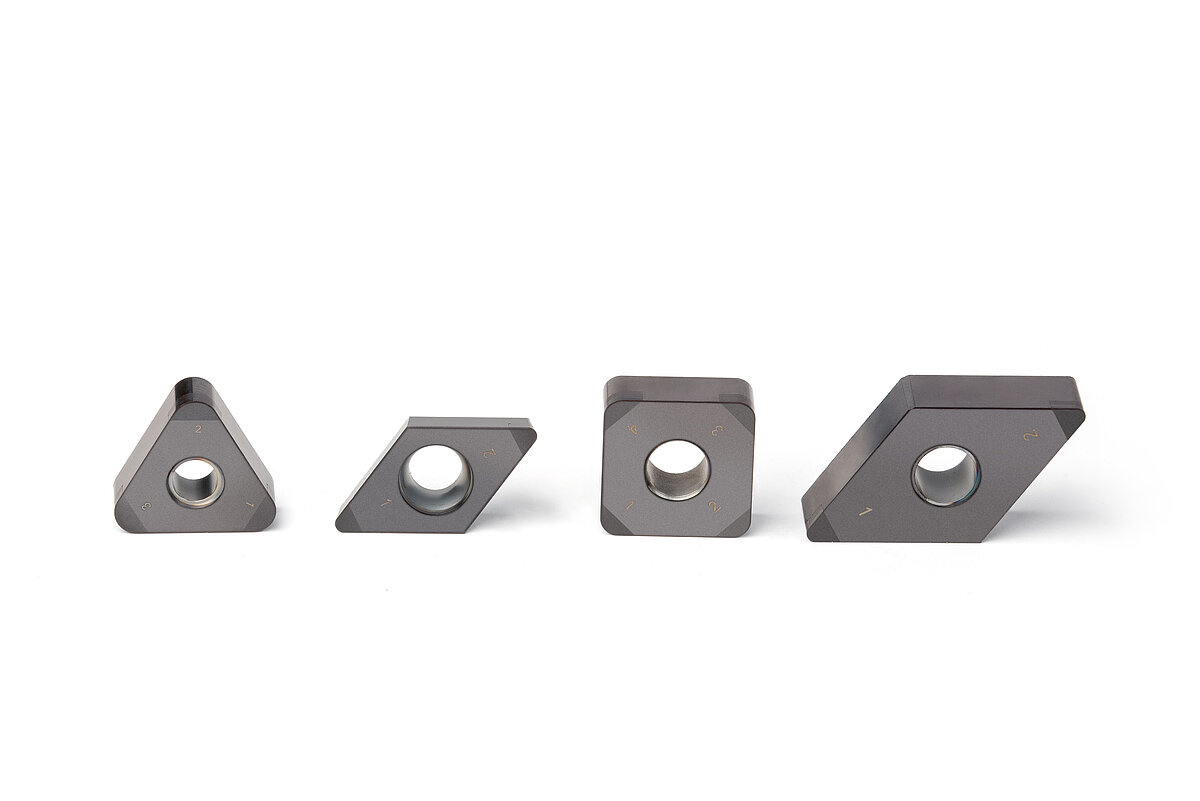
New PcBN cutting materials for continuous and interrupted cuts achieve significant increases in tool life when hard turning drive joints
Five-cutting-edge milling cutter design reduces machining time and unit costs
This does not yet take into account the impact of a new, five-cutting-edge tool design for ball-track milling cutters, which MAPAL is also set to launch in 2026. To date, four-cutting-edge designs have been the state of the art in practice. The additional cutting edge reduces machining time by around 20 per cent compared with the four-edge design. The engagement time per cutting edge for each ball-track is reduced, which also has a positive effect on tool life in applications. With annual production volumes of around 15 million components, these two effects combined offer significant potential for savings in terms of unit costs.
New cutting materials also deliver a significant improvement in hard turning
MAPAL has also introduced new PcBN cutting materials for hard turning, with the initial focus here too on machining drive joints. The FP240 grade is designed for smooth-cutting applications, such as on the shaft of the outer race. For interrupted cuts, such as those encountered on the inner race and the cage, the tougher FP260 grade is used. Both are PVD-coated and achieve a tool life that is a good 40 per cent longer than that of conventional cutting materials.
The phased introduction of ball-track milling cutters and PcBN turning inserts underlines MAPAL’s commitment to consistently raising the benchmark in the machining of hardened components.
Source | MAPAL