Plastics Machining for Chip Manufacturing
The core business of M-O-T Mikro- und Oberflächentechnik GmbH in Saarbrücken is the manufacture of equipment for producing microchips. In its efforts to manufacture as many of the necessary plastic parts in-house as possible, the company has made significant progress by using the MAPAL NeoMill Diamond FlyCutter.
Founded in 2001, M-O-T Mikro- und Oberflächentechnik GmbH has been part of the Woll Group since 2011 and complements the diverse special-purpose machinery manufacturer’s product portfolio with the production of wet chemical processing systems for the microsystems and semiconductor sectors. With just under 30 employees, the specialist is fully integrated into the group, a fact that is also evident in its physical location: M-O-T occupies three rooms in the middle of a Woll production hall.
In this area, some things are different from the rest of the production facilities, which are primarily focused on metalworking. Outdoor shoes are not permitted here, and there is a constant slight overpressure. Although manufacturing does not take place in a cleanroom, it does occur in a controlled-environment room, as Production Manager Mike Jakob explains. Contaminants carried in could alter values in the precision equipment and thus jeopardize the process. At the customers’ sites, operations later take place in cleanrooms.
Apart from the built-in electronics, the systems are made almost entirely of plastic and are designed modularly for the individual process steps required sequentially in semiconductor manufacturing. Process cells are lined up along the front, into which silicon wafers are loaded for processing. Behind the machine are storage tanks containing the necessary liquids, mostly acids, bases, and solvents. Electroplating is also possible if needed. Depending on the application, surface treatment takes place on M-O-T’s custom-designed systems either before or after the wafers are exposed. With purchased components, photolithography can also be integrated directly into the system.
Plastics Based on Their Intended Use
To manufacture the containers used in chemical processing and storage, M-O-T primarily uses sheets that are welded together using a thermal joining process. Various plastics are used in this process, and the selection of the appropriate material depends on the specific chemicals and the process temperature. PP or PVC is usually used, but in some cases, high-temperature-resistant PEEK or completely acid-resistant PVDF is required. When several extreme requirements come together, PTFE—also known as Teflon—is often the best choice.
The number of systems built has risen sharply in recent years. While the figure was five to six per year in 2021, M-O-T now delivers 20 to 30. However, there are fluctuations depending on market conditions, which in turn depend on developments in the global semiconductor market. In addition, the systems are becoming more complex. Initially, production relied primarily on suppliers. The fact that M-O-T has been relying on in-house production since 2022 is also linked to quality issues with the supplied parts: Leaks had repeatedly occurred in finished systems.
The way M-O-T processes its plastic panels seems curious at first glance: the machine comes from the model-making industry, the tool was developed for milling aluminum, and the cooling lubricant (KSS) is actually a disinfectant. For the purposes of the Saarbrücken-based equipment manufacturer, however, this unusual combination is quite effective.
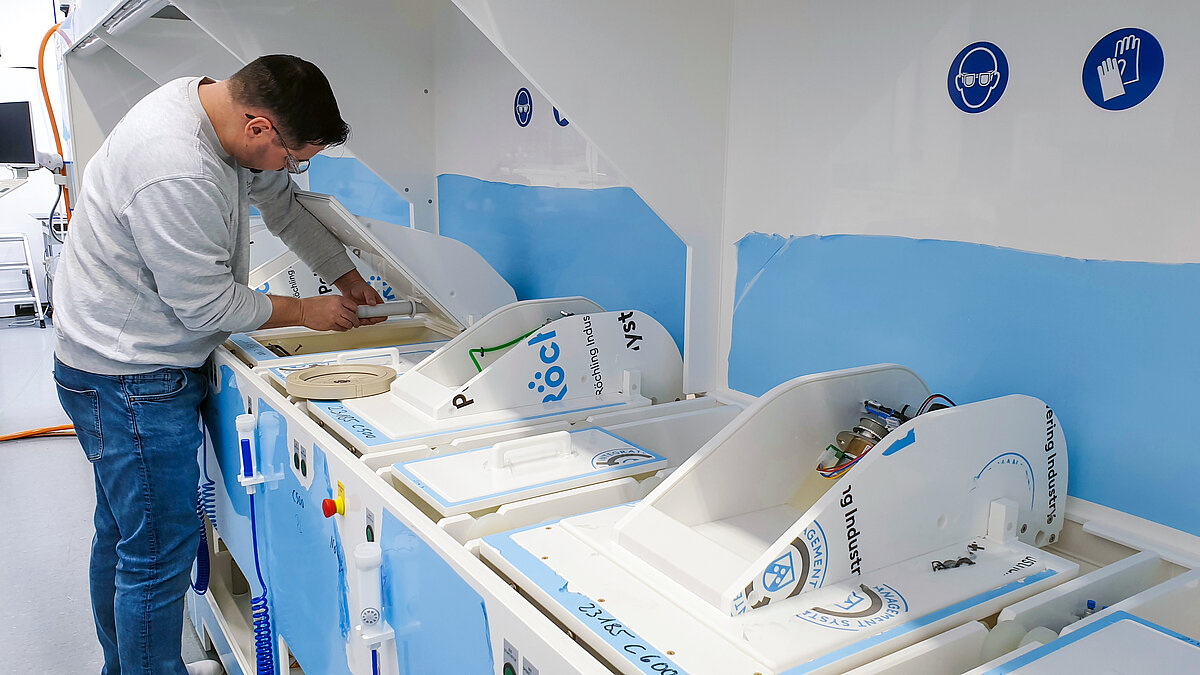
Production Manager Mike Jakob demonstrates how work is carried out at the plant's process cells.
After a year of searching, the NeoMill Diamond FlyCutter offers the solution
The machine selected was the T-Rex open-gate milling machine from CNC-Step. A small SK30 tool holder is used, and workpieces up to 1,000 x 1,000 mm in size can be clamped onto the vacuum table. Finding a suitable tool for the intended machining operations—which primarily focus on achieving a high-quality surface finish—proved to be a challenge. Mike Jakob reports: “We weren’t satisfied with the quality we achieved at the beginning. I spent a year looking for a suitable cutter head, but no one could offer us anything that was truly suitable for the surface finish. At AMB 2024 in Stuttgart, I found what I was looking for at MAPAL, where they had a milling cutter with our mounting.”
Together with application engineer Klaus-Dieter Leick from MAPAL, they worked out the best feasible solution for the existing machine. The choice fell on a NeoMill Diamond FlyCutter with a 63 mm milling head diameter. “We originally developed this tool for machining aluminum components in the electronics industry, where the goal was to achieve the most perfect possible surfaces during face milling,” reports Leander Bolz from MAPAL’s Component Management department. The tool manufacturer from Aalen was immediately confident that this would also work with plastic, especially since the tool was designed from the outset for critical machine configurations such as small spindles and vacuum clamping.
With its special cutting geometry, the lightweight, three-fluted milling cutter reduces cutting pressure and removes chips relatively quickly from the cutting zone. The low cutting pressure was already a decisive factor when milling aluminum surfaces. By selecting the appropriate cutting material, MAPAL can adapt the tool to different materials.
M-O-T is very satisfied with the now widely used NeoMill Diamond FlyCutter, which has proven to be a true game-changer in surface finishing. When the milling machine was purchased, the manufacturers initially had only the machining of doors for cabinet bodies in mind. Gradually, however, more and more components came from their own production. M-O-T now manufactures the storage tanks for the required chemicals entirely in-house and plans to produce the process cells on its own in the future as well. Special components, such as Teflon process tanks, will continue to be manufactured externally. M-O-T uses the NeoMill Diamond FlyCutter for face milling the plates. For side machining and finishing contours, another MAPAL tool—a PCD end mill—is used.
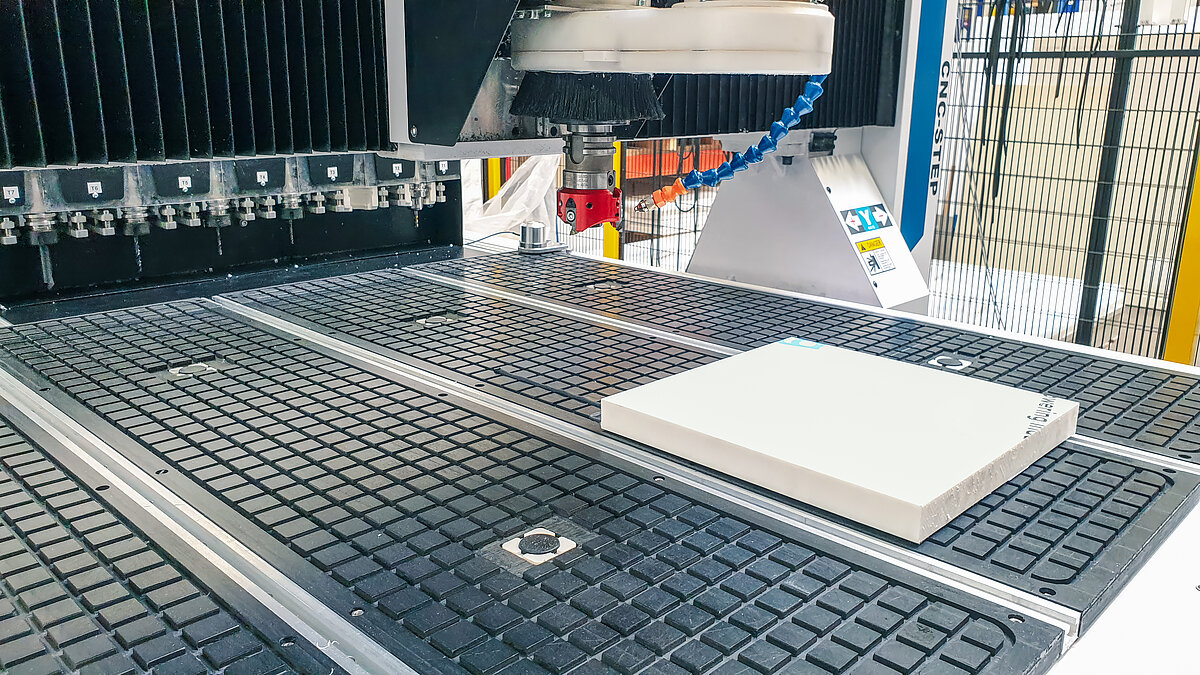
The M-O-T can use a vacuum to clamp components up to 1,000 x 1,000 mm onto the machine's worktable. With its low cutting pressure, the NeoMill Diamond FlyCutter from MAPAL is ideal for milling the plates.

MAPAL's lightweight HSC NeoMill-Diamond-FlyCutter is ideal for machining the surfaces of plastic parts in a BT30 holder, which M-O-T clamps onto a vacuum table.
Optimization will continue
Mike Jakob’s department does not yet consider itself to have fully achieved its goal. Further experimentation with the cooling lubricant is planned to optimize surface quality and minimize wear on the tool. In particular, machining the rigid and brittle PVDF has at times taken a toll on the PCD cutting edges of the NeoMill Diamond FlyCutter. However, M-O-T faces significant limitations in its choice of coolant. Oil is out of the question to prevent contaminants from entering the system—contaminants that could, for example, affect the pH value or other process parameters. For this reason, metal chips must not enter M-O-T’s production area either. Because it evaporates very quickly, isopropanol was chosen as the coolant. However, since it produces a significant odor, its use on the machine is limited.
Plastics also pose special challenges when it comes to cooling, as Robin Kollmann, who is responsible for milling at M-O-T, explains: “Plastic absorbs less heat than aluminum, so the heat cannot be dissipated from the component quickly enough. The chips can fuse together or clump, which builds up more pressure and potentially damages the cutting edge. The surface quality is also not as good as we would like it to be.” During machining, 0.3 mm is removed per cut. Depending on the material and grade, the allowance is up to 1 mm.
To avoid generating too much heat during machining, M-O-T is currently operating at a cutting speed of 6,000 rpm and a feed rate of 1,200 mm/min. This keeps the machining parameters well below the values initially proposed by MAPAL, which were already set lower than those for aluminum machining. Not enough data has yet been collected to assess the impact of isopropanol cooling on the cutting edge’s service life. At the same time, M-O-T has begun testing a new water-based coolant. As part of these trials, the machinists also plan to test higher cutting speeds.
In the meantime, the next optimization step has been successfully tested: M-O-T tested a larger version of the NeoMill Diamond FlyCutter with a 100-mm milling head diameter and subsequently ordered the tool. The changeover is possible with minimal effort in the modular system, as all milling head diameters offered by MAPAL—ranging from 63 to 160 mm—are mounted on the same shank. This clearly demonstrates that MAPAL not only supports the application with a suitable tool but also develops further approaches to increasing productivity through continuous dialogue with the customer.

Group photo at the machine: (front, from left) Robin Kollmann (Milling M-O-T), Mike Jakob (Production Manager M-O-T), (back, from left) Jan Schattschneider (Milling & Production Center M-O-T), Klaus-Dieter Leick (MAPAL Application Engineering), and Leander Bolz (Component Management MAPAL).
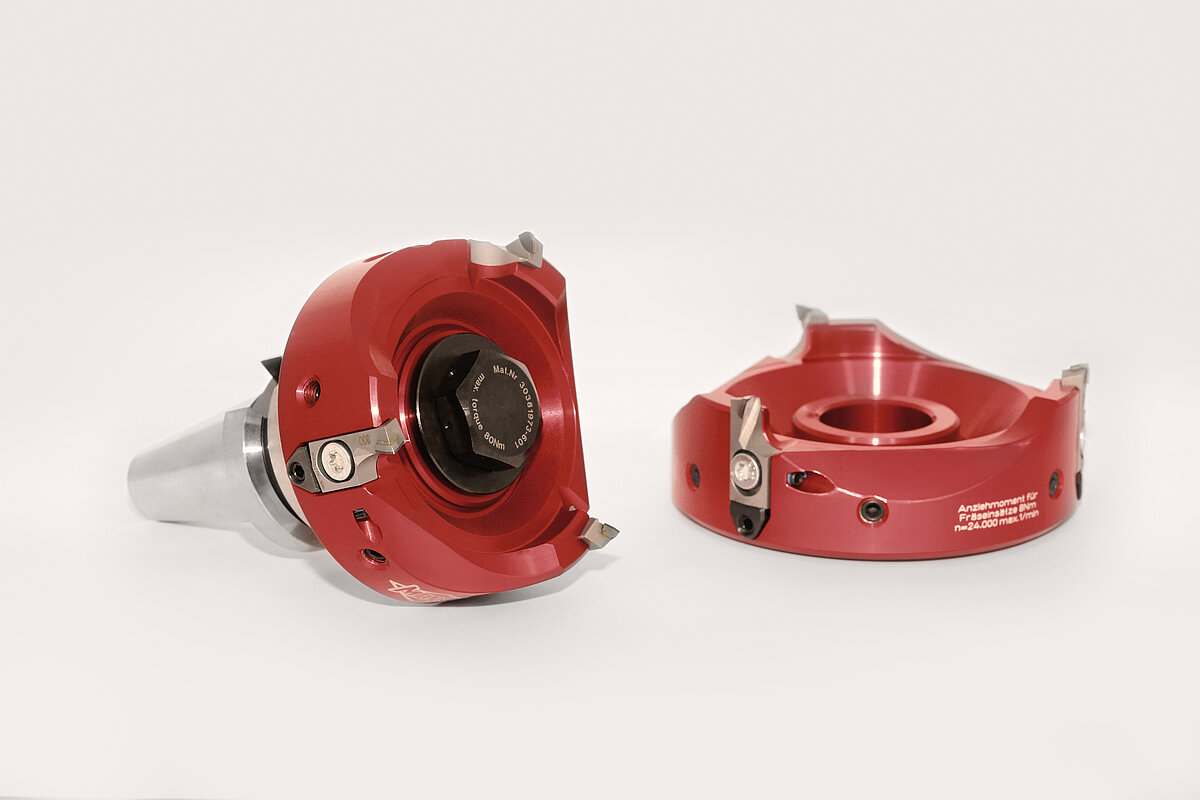
The three-fluted NeoMill Diamond FlyCutter with PCD-tipped milling inserts was specifically designed for delicate machining operations and small cutting areas.
Brief Profile of MAPAL Dr. Kress SE & Co. KG: MAPAL Tools for Customer Success
MAPAL Dr. Kress SE & Co. KG is one of the world’s leading suppliers of precision cutting tools for machining virtually all materials. Founded in 1950, the company supplies renowned customers primarily in the automotive and aerospace industries, mechanical and plant engineering, and tool and mold making. With its innovations, the family-owned company sets trends and standards in manufacturing and machining technology. MAPAL sees itself as a technology partner that supports its customers in developing efficient and resource-conserving machining processes with customized tool concepts. The company is represented in 42 countries through production and sales locations as well as service partners. The MAPAL Group employs 4,500 people; in 2025, its revenue totaled 514 million euros.
Source |MAPAL Dr. Kress SE & Co. KG